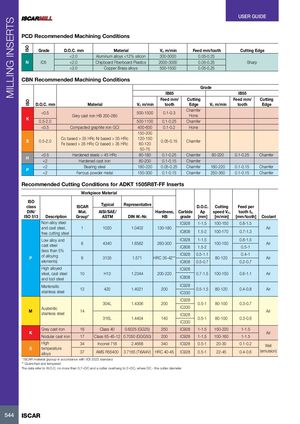
PCD Recommended Machining Conditions
| ISO | Grade | D.O.C. mm | Material | Vc m/min | Feed mm/tooth | Cutting Edge |
| | | Aluminum alloys | 300-3000 | 0.05-0.25 | |
| N | ID5 | | Chipboard Fiberboard Plastics | 2000-3000 | 0.05-0.25 | Sharp |
| | | Copper Brass alloys | 500-1500 | 0.05-0.25 | |
CBN Recommended Machining Conditions
| | | | | Gr | ade | | |
| | | | IB85 | | | IB55 | |
| ISO D. | O.C. mm | Material | Vc m/min | Feed mm/ tooth | Cutting Edge | Vc m/min | Feed mm/ tooth | Cutting Edge |
| | Grey cast iron HB 200-280 | 500-1500 | 0.1-0.3 | Chamfer Hone | | | |
| K 0 | .5-2.0 | | 500-1100 | 0.1-0.25 | Chamfer | | | |
| | Compactedgraphite iron GCI | 400-600 | 0.1-0.2 | Hone | | | |
| S 0 | .5-2.0 | Co based > 35 HRc Ni based > 35 HRc Fe based > 35 HRc Cr based > 35 HRc | 150-200 120-150 60-120 50-75 | 0.05-0.15 | Chamfer | | | |
| H | | Hardened steels > 45 HRc | 80-180 | 0.1-0.25 | Chamfer | 80-220 | 0.1-0.25 | Chamfer |
| | Hardened cast iron | 80-200 | 0.1-0.15 | Chamfer | | | |
| P | | Bearingsteel | 180-220 | 0.05-0.25 | Chamfer | 180-220 | 0.1-0.15 | Chamfer |
| | Ferrouspowder metal | 150-300 | 0.1-0.15 | Chamfer | 250-360 | 0.1-0.15 | Chamfer |
Recommended Cutting Conditions for ADKT 1505R8T-FF Inserts
| ISO class | | Workp ISCAR | iece Material Typical | Representative | | | D.O.C. | Cutting | Feed per | |
| DIN/ ISO 513 | Description | Mat. Group | AISI/SAE/ ASTM | DIN W.-Nr. | Hardness, HB | Carbide grade | Ap [mm] | speed Vc, [m/min] | tooth fz, [mm/tooth] | Coolant |
| Non-alloy steel | | | | | IC928 | 1-1.5 | 100-150 | 0.8-1.5 | |
| and cast steel, | 1 | 1020 | 1.0402 | 130-180 | | | | | Air |
| free cuttingsteel | | | | | IC808 | 1.5-2 | 100-170 | 0.7-1.3 | |
| Low alloy and | 8 | 4340 | 16582 | 260-300 | IC928 | 1-1.5 | 100-150 | 0.8-1.5 | Air |
| cast steel l th 5% | | | . | | IC808 | 1.5-2 | | 0.5-1 | |
| P | (ess an of alloying | 9 | 3135 | 1.571 | HRC 35-42 | IC928 | 0.5-1.1 | 80-120 | 0.4-1 | Air |
| elements) | | | | | IC808 | 0.5-0.7 | | 0.2-0.7 | |
| High alloyed steel, cast steel and tool steel | 10 | H13 | 1.2344 | 200-220 | IC928 IC808 | 0.7-1.5 | 100-150 | 0.6-1.1 | Air |
| Martensitic stainless steel | 12 | 420 | 1.4021 | 200 | IC928 IC330 | 0.5-1.5 | 80-120 | 0.4-0.8 | Air |
| M | Austenitic | 14 | 304L | 1.4306 | 200 | IC928 IC330 | 0.5-1 | 80-100 | 0.3-0.7 | Air |
| stainless steel | | 316L | 1.4404 | 140 | IC928 IC330 | 0.5-1 | 80-100 | 0.3-0.6 | |
| K | Grey cast iron | 16 | Class 40 | 0.6025 (GG25) | 250 | IC928 | 1-1.5 | 150-220 | 1-1.5 | Air |
| Nodular cast iron | 17 | Class 65-45-12 | 0.7050 (GGG50) | 200 | IC928 | 1-1.5 | 100-160 | 1-1.5 | |
| High | 34 | Inconel 718 | 2.4668 | 340 | IC928 | 0.5-1 | 20-30 | 0.1-0.2 | Wet |
| S | temperature alloys | 37 | AMS R56400 | 3.7165 (Ti6Al4V) | HRC 40-45 | IC928 | 0.5-1 | 22-45 | 0.4-0.6 | (emulsion) |
* ISCAR material grpoup in accordance with VDI 3323 standard ** Quenched and tempered The data refer to W.O.C. no more than 0.7×DC and a cutter overhang to 2×DC, where DC - the cutter diameter
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления