Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 163
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
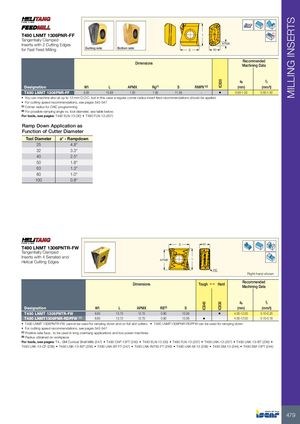
| T490 LNMT 1306PNR-FF | L | Rd° | |
| Tangentially Clamped | |||
| Inserts with 2 Cutting Edges | APMX |
for Fast Feed Milling S W
1 Recommended Dimensions Machining Data
a f p z
| Designation | W1 | L | APMX | Rg(1) | S | RMPX°(2) | (mm) | (mm/t) | ||
| T490 LNMT 1306PNR-FF | 6.65 | 13.68 | 1.00 | 1.95 | 11.56 | - | • | 0.60-1.00 | 0.50-1.50 |
- You can machine also at up to 12 mm D.O.C. but in this case a regular corner radius insert feed recommendations should be applied.
- For cutting speed recommendations, see pages 542-547
(1) Corner radius for CNC programming (2) For possible ramping angle vs. tool diameter, see table below.
For tools, see pages: T490 ELN-13 (30) T490 FLN-13 (207)
Ramp Down Application as
Function of Cutter Diameter
| Tool Diameter | a° - Rampdown |
| 25 | 4.8° |
| 32 | 3.3° |
| 40 | 2.5° |
| 50 | 1.8° |
| 63 | 1.3° |
| 80 | 1.0° |
| 100 | 0.8° |
S W1 T490 LNMT 1306PNTR-FW Tangentially Clamped Inserts with 4 Serrated and L Helical Cutting Edges APMX RE Right-hand shown Recommended
Dimensions Tough 1 Hard
Machining Data
a p fz
| Designation | W1 | L | APMX | RE(2) | S | (mm) | (mm/t) | ||
| T490 LNMT 1306PNTR-FW | 6.65 | 13.73 | 12.70 | 0.80 | 13.06 | • | 4.00-12.00 | 0.10-0.20 | |
| T490 LNMT1306PNR-RDPFW (1) | 6.65 | 13.73 | 12.70 | 0.80 | 13.06 | • | 4.00-12.00 | 0.10-0.18 |
- T490 LNMT 1306PNTR-FW cannot be used for ramping down and on full slot cutters
- T490 LNMT1306PNR-RDPFW can be used for ramping down
- For cutting speed recommendations, see pages 542-547
(1) Positive rake face, to be used in long overhang applications and low power machines (2) Radius obtained on workpiece
For tools, see pages: T4..-SM Conical Shell Mills (247) T490 CAP-13FT (245) T490 ELN-13 (30) T490 FLN-13 (207) T490 LNK-13 (237) T490 LNK-13-BT (238) T490 LNK-13-CF (238) T490 LNK-13-INT (238) T490 LNK-BT-FT (247) T490 LNK-INT50-FT (246) T490 LNK-M-13 (238) T490 SM-13 (244) T490 SM-13FT (244)