Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 124
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
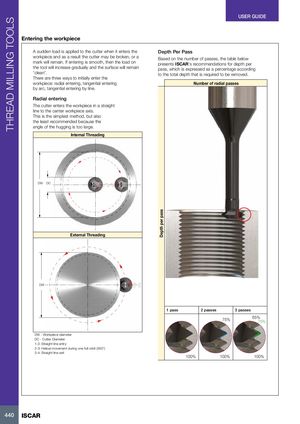
Entering the workpiece
| A sudden load is applied to the cutter when it enters the | Depth Per Pass |
| workpiece and as a result the cutter may be broken, or a | Based on the number of passes, the table below |
| mark will remain. If entering is smooth, then the load on | presents ISCAR's recommendations for depth per |
| the tool will increase gradually and the surface will remain | pass, which is expressed as a percentage according |
| “clean”. | to the total depth that is required to be removed. |
There are three ways to initially enter the workpiece: radial entering, tangential entering Number of radial passes by arc, tangential entering by line. Radial entering
The cutter enters the workpiece in a straight line to the center workpiece axis. This is the simplest method, but also the least recommended because the angle of the hugging is too large. Internal Threading
DW DC 1 2
4 3
External Threading
DW 2 1
3 4
DC 1 pass
2 passes
3 passes 65% 75% 75%
DW - Workpiece diameter DC - Cutter Diameter 1-2: Straight line entry 2-3: Helical movement during one full orbit (360°) 3-4: Straight line exit
100% 100% 100%