Каталог Iscar инструмент для внутренней обработки - страница 129
Навигация
 Каталог Iscar инструментальные блоки
 Фрезерные инструменты Iscar 2026
 Каталог Iscar обработка канавок 2022
 Каталог Iscar инструмент для нарезания резьбы
 Токарные инструменты Iscar (часть 2) 2026
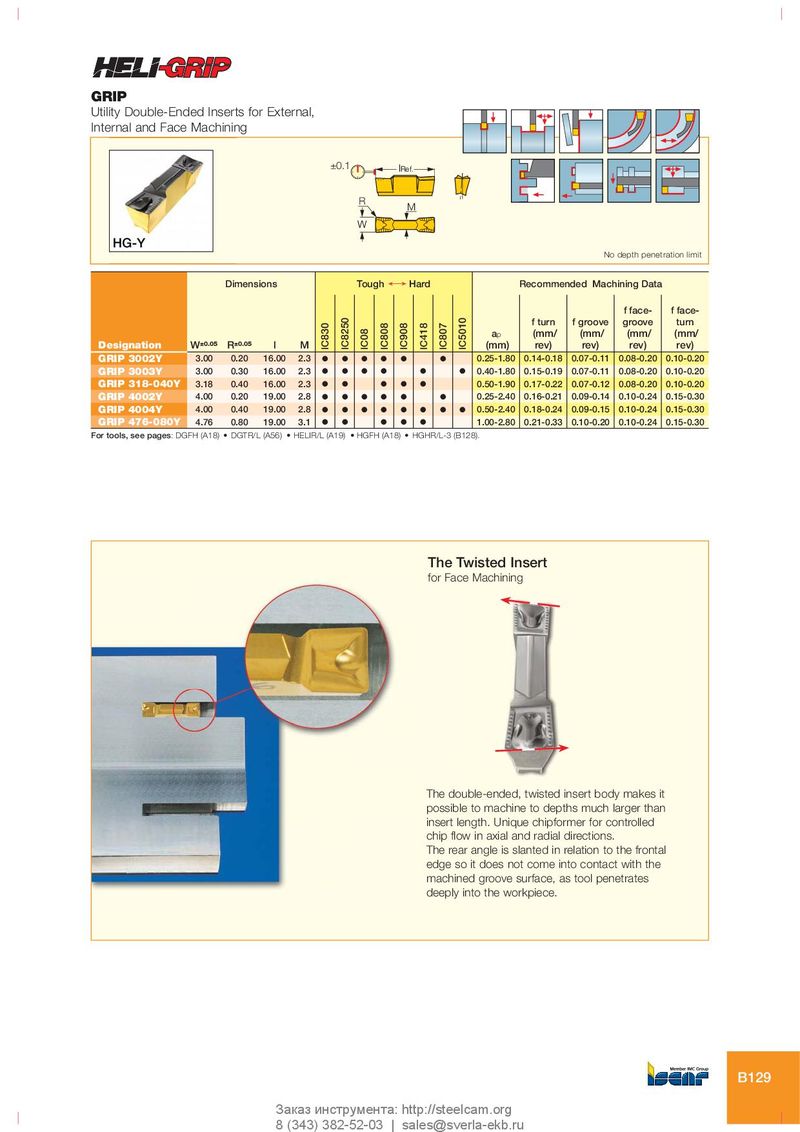
GRIP
Utility Double-Ended Inserts for External,
Internal and Face Machining
±0.1 l Ref.
R M W
No depth penetration limit
| Dimensions | Tough ¥ Hard | Recommended Machining Data | ||
| f face- | f face- |
| f turn | f groove | groove | turn | |||||||||||||||
| ap | (mm/ | (mm/ | (mm/ | (mm/ | ||||||||||||||
| Designation | W±0.05 | R ±0.05 | l | M | (mm) | rev) | rev) | rev) | rev) | |||||||||
| GRIP 3002Y | 3.00 | 0.20 | 16.00 | 2.3 | O | O | O | O | O | O | 0.25-1.80 | 0.14-0.18 | 0.07-0.11 | 0.08-0.20 | 0.10-0.20 | |||
| GRIP 3003Y | 3.00 | 0.30 | 16.00 | 2.3 | O | O | O | O | O | O | 0.40-1.80 | 0.15-0.19 | 0.07-0.11 | 0.08-0.20 | 0.10-0.20 | |||
| GRIP 318-040Y | 3.18 | 0.40 | 16.00 | 2.3 | O | O | O | O | O | 0.50-1.90 | 0.17-0.22 | 0.07-0.12 | 0.08-0.20 | 0.10-0.20 | ||||
| GRIP 4002Y | 4.00 | 0.20 | 19.00 | 2.8 | O | O | O | O | O | O | 0.25-2.40 | 0.16-0.21 | 0.09-0.14 | 0.10-0.24 | 0.15-0.30 | |||
| GRIP 4004Y | 4.00 | 0.40 | 19.00 | 2.8 | O | O | O | O | O | O | O | O | 0.50-2.40 | 0.18-0.24 | 0.09-0.15 | 0.10-0.24 | 0.15-0.30 | |
| GRIP 476-080Y | 4.76 | 0.80 | 19.00 | 3.1 | O | O | O | O | O | 1.00-2.80 | 0.21-0.33 | 0.10-0.20 | 0.10-0.24 | 0.15-0.30 |
For tools, see pages: DGFH (A18) • DGTR/L (A56) • HELIR/L (A19) • HGFH (A18) • HGHR/L-3 (B128).
The Twisted Insert
for Face Machining
The double-ended, twisted insert body makes it
possible to machine to depths much larger than
insert length. Unique chipformer for controlled
chip flow in axial and radial directions.
The rear angle is slanted in relation to the frontal
edge so it does not come into contact with the
machined groove surface, as tool penetrates
deeply into the workpiece.