Брошюра Dormer Pramet новинки 2021 - страница 23
Навигация
 Общий каталог Dormer Pramet 2016
 Каталог Dormer Pramet обработка отверстий 2021 - 2022
 Каталог Dormer Pramet фрезерование 2021 - 2022
 Общий каталог Dormer Pramet 2017
 Каталог оснастка Dormer Pramet 2016
 Каталог Dormer Pramet обработка резьбы 2021 - 2022
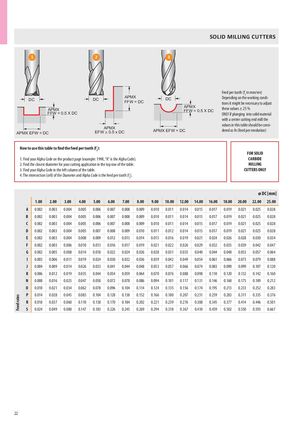
HM Milling with ≥ 50% radial immersion
1 2 3
Feed per tooth (f in mm/rev) APMX z
DC DC DC Depending on the working condi-
FFW = DC tions it might be necessary to adjust APMX these values ± 25 % APMX FFW = 0.5 X DC FFW = 0.5 X DC ONLY if plunging into solid material
with a center cutting end mill the values in this table should be consi- APMX
| EFW ≥ 0.5 x DC | dered as fn (feed per revolution) APMX EFW = DC | |
| APMX EFW = DC | ||
| How to use this table to find the feed per tooth (f ): | ||
| z | FOR SOLID | |
| 1. Find your Alpha Code on the product page (example: 199K, “K“ is the Alpha Code). | CARBIDE | |
| 2. Find the closest diameter for your cutting application in the top row of the table. | MILLING | |
| 3. Find your Alpha Code in the left column of the table. | CUTTERS ONLY |
4. The intersection (cell) of the Diameter and Alpha Code is the feed per tooth (f ). z
| ø D | C [mm] | ||||||||||||||||
| 1.00 | 2.00 | 3.00 | 4.00 | 5.00 | 6.00 | 7.00 | 8.00 | 9.00 | 10.00 | 12.00 | 14.00 | 16.00 | 18.00 | 20.00 | 22.00 | 25.00 | |
| A | 0.002 | 0.003 | 0.004 | 0.005 | 0.006 | 0.007 | 0.008 | 0.009 | 0.010 | 0.011 | 0.014 | 0.015 | 0.017 | 0.019 | 0.021 | 0.025 | 0.028 |
| B | 0.002 | 0.003 | 0.004 | 0.005 | 0.006 | 0.007 | 0.008 | 0.009 | 0.010 | 0.011 | 0.014 | 0.015 | 0.017 | 0.019 | 0.021 | 0.025 | 0.028 |
| C | 0.002 | 0.003 | 0.004 | 0.005 | 0.006 | 0.007 | 0.008 | 0.009 | 0.010 | 0.011 | 0.014 | 0.015 | 0.017 | 0.019 | 0.021 | 0.025 | 0.028 |
| D | 0.002 | 0.003 | 0.004 | 0.005 | 0.007 | 0.008 | 0.009 | 0.010 | 0.011 | 0.012 | 0.014 | 0.015 | 0.017 | 0.019 | 0.021 | 0.025 | 0.028 |
| E | 0.002 | 0.003 | 0.004 | 0.008 | 0.009 | 0.012 | 0.013 | 0.014 | 0.015 | 0.016 | 0.019 | 0.021 | 0.024 | 0.026 | 0.028 | 0.030 | 0.034 |
| F | 0.002 | 0.003 | 0.006 | 0.010 | 0.013 | 0.016 | 0.017 | 0.019 | 0.021 | 0.022 | 0.026 | 0.029 | 0.032 | 0.035 | 0.039 | 0.042 | 0.047 |
| G | 0.002 | 0.005 | 0.008 | 0.014 | 0.018 | 0.022 | 0.024 | 0.026 | 0.028 | 0.031 | 0.035 | 0.040 | 0.044 | 0.048 | 0.053 | 0.057 | 0.064 |
| I | 0.003 | 0.006 | 0.011 | 0.019 | 0.024 | 0.030 | 0.032 | 0.036 | 0.039 | 0.042 | 0.049 | 0.054 | 0.061 | 0.066 | 0.073 | 0.079 | 0.088 |
| J | 0.004 | 0.009 | 0.014 | 0.026 | 0.033 | 0.041 | 0.044 | 0.048 | 0.053 | 0.057 | 0.066 | 0.074 | 0.083 | 0.090 | 0.099 | 0.107 | 0.120 |
| K | 0.006 | 0.012 | 0.019 | 0.035 | 0.044 | 0.054 | 0.059 | 0.064 | 0.070 | 0.076 | 0.088 | 0.098 | 0.110 | 0.120 | 0.132 | 0.142 | 0.160 |
| N | 0.008 | 0.016 | 0.025 | 0.047 | 0.058 | 0.072 | 0.078 | 0.086 | 0.094 | 0.101 | 0.117 | 0.131 | 0.146 | 0.160 | 0.175 | 0.189 | 0.212 |
| O | 0.010 | 0.021 | 0.034 | 0.062 | 0.078 | 0.096 | 0.104 | 0.114 | 0.124 | 0.135 | 0.156 | 0.174 | 0.195 | 0.213 | 0.233 | 0.252 | 0.283 |
| P tes | 0.014 | 0.028 | 0.045 | 0.083 | 0.104 | 0.128 | 0.138 | 0.152 | 0.166 | 0.180 | 0.207 | 0.231 | 0.259 | 0.283 | 0.311 | 0.335 | 0.376 |
| R d ra | 0.018 | 0.037 | 0.060 | 0.110 | 0.138 | 0.170 | 0.184 | 0.202 | 0.221 | 0.239 | 0.276 | 0.308 | 0.345 | 0.377 | 0.414 | 0.446 | 0.501 |
| S Fee | 0.024 | 0.049 | 0.080 | 0.147 | 0.183 | 0.226 | 0.245 | 0.269 | 0.294 | 0.318 | 0.367 | 0.410 | 0.459 | 0.502 | 0.550 | 0.593 | 0.667 |