Общий каталог Dijet 2018 - страница 53
Навигация
 Общий каталог Dijet 2012 на русском
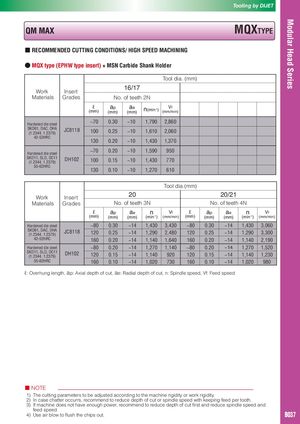
■ RECOMMENDED CUTTING CONDITIONS/ HIGH SPEED MACHINING
- MQX type (EPHW type insert) + MSN Carbide Shank Holder
| Tool dia | .(mm) | ||||||||||
| Work | Insert | 16/17 | |||||||||
| Materials | Grades | No. | of teeth | 2N | |||||||
| ℓ (mm) | ap (mm) | ae (mm) | n(min-1) | Vf (mm/min) | |||||||
| Hardened die steel | ~70 | 0.30 | ~10 | 1,790 | 2,860 | ||||||
| SKD61, DAC, DHA (1.2344, 1.2379) | JC8118 | 100 | 0.25 | ~10 | 1,610 | 2,060 | |||||
| 42-52HRC | 130 | 0.20 | ~10 | 1,430 | 1,370 | ||||||
| Hardened die steel | ~70 | 0.20 | ~10 | 1,590 | 950 | ||||||
| SKD11, SLD, DC11 (1.2344, 1.2379) | DH102 | 100 | 0.15 | ~10 | 1,430 | 770 | |||||
| 55-62HRC | 130 | 010 | ~10 | 1270 | 610 | ||||||
| . | , | Tool dia | .(mm) | ||||||||
| Work | Insert | 20 | 20/21 | ||||||||
| Materials | Grades | No. | of teet | h3N | No. | of teeth | 4N | ||||
| ℓ (mm) | ap (mm) | ae (mm) | n (min-1) | Vf (mm/min) | ℓ (mm) | ap (mm) | ae (mm) | n (min-1) | Vf (mm/min) | ||
| Hardened die steel | ~80 | 0.30 | ~14 | 1,430 | 3,430 | ~80 | 0.30 | ~14 | 1,430 | 3,060 | |
| SKD61, DAC, DHA (1.2344 1.2379) | JC8118 | 120 | 0.25 | ~14 | 1,290 | 2,480 | 120 | 0.25 | ~14 | 1,290 | 3,300 |
| , 42-52HRC | 160 | 0.20 | ~14 | 1,140 | 1,640 | 160 | 0.20 | ~14 | 1,140 | 2,190 | |
| Hardened die steel | ~80 | 0.20 | ~14 | 1,270 | 1,140 | ~80 | 0.20 | ~14 | 1,270 | 1,520 | |
| SKD11, SLD, DC11 (1.2344, 1.2379) | DH102 | 120 | 0.15 | ~14 | 1,140 | 920 | 120 | 0.15 | ~14 | 1,140 | 1,230 |
| 55-62HRC | 160 | 0.10 | ~14 | 1,020 | 730 | 160 | 0.10 | ~14 | 1,020 | 980 |
ℓ: Overhung length, ap: Axial depth of cut, ae: Radial depth of cut, n: Spindle speed, Vf: Feed speed