Общий каталог Dijet 2018 - страница 45
Навигация
 Общий каталог Dijet 2012 на русском
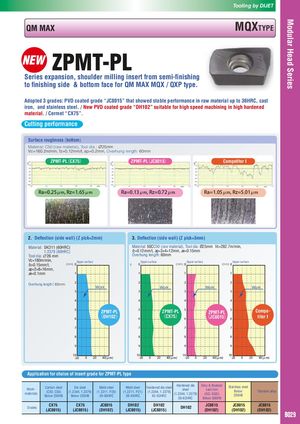
ZPMT-PL
Series expansion, shoulder milling insert from semi-finishing
to finishing side & bottom face for QM MAX MQX / QXP type.
Adopted 3 grades: PVD coated grade “JC8015” that showed stable performance in raw material up to 36HRC, cast
iron, and stainless steel. / New PVD coated grade “DH102” suitable for high speed machining in high hardened
material. / Cermet “CX75”.
Cutting performance
Surface roughness (bottom)
Material: C50 (raw material), Tool dia.: Ø25mm
Vc=160.2m/min, fz=0.12mm/t, ap=0.2mm, Overhung length: 60mm
ZPMT-PL(CX75) ZPMT-PL(JC8015) Competitor I
Ra=0.25μm, Rz=1.65μm Ra=0.13μm, Rz=0.72μm Ra=1.05μm, Rz=5.01μm
| 2. Deflection (side wall) (Z pick=2mm) | 3. Deflection (side wall) (Z pick=3mm) |
| Material: SKD11 (60HRC) | Material: 50CC50 (raw material), Tool dia: Ø25mm Vc=282.7m/min, |
| 1.2379 (60HRC) fz=0.12mm/t, ap=3×4=12mm, ae=0.15mm | |
| Tool dia: Ø 26 mm | Overhung length: 60mm |
| Vc=180m/min, | |
| Upper surface Upper surface Upper surface Upper surface |
| fz=0.15mm/t, | (mm) 0 | ç | 0 | (mm) 0 | (mm) 0 | ||||
| ap=2×8=16mm, | |||||||||
| ae=0.1mm | 1 | 1 | 1 | 1 | |||||
| : | 2 | 2 | 2 | 2 | |||||
| Overhung length | 65mm |
Work Work Work Work
| 3 | 3 | 3 | 3 | |||
| 4 | 4 | 4 | 4 | |||
| 5 | 5 | ZPMT-PL 5 | 5 | Compe- | ||
| ZPMT-PL | ZPMT-PL | |||||
| (DH102) | (CX75) | ( | ) | titor I | ||
| 6 | 6 | 6 | JC8015 | 6 | ||
| 7 | 7 | 7 | 7 | |||
| 8 | 8 | 8 | 8 | |||
| 9 | 9 | 9 | 9 | |||
| 10 | 10 | 10 | 10 | |||
| -20 | 20 0 40(μm) | -20 | 40(μm) 20 0 -20 | 20 0 40(μm) | -20 | 20 0 40(μm) |
Application for choice of insert grade for ZPMT-PL type
| Work- materials | Carbon steel (C50, C55) Below 250HB | Die steel (1.2344, 1.2379) Below 255HB | Mold steel (1.2311, P20) 30-36HRC | Mold steel (1.2311, P21) 38-43HRC | Hardened die steel (1.2344, 1.2379) 42-52HRC ( | Hardened die steel 1.2344, 1.2379) 55-62HRC | Grey & Nodular cast iron (GG, GGG) Below 300HB | Stainless steel Below 250HB | Titanium alloy |
| Grades | CX75 (JC8015) | CX75 (JC8015) | JC8015 (DH102) | DH102 (JC8015) | DH102 (JC8015) | DH102 | JC8015 (DH102) | JC8015 (DH102) | JC8015 (DH102) |