Общий каталог Dijet 2018 - страница 43
Навигация
 Общий каталог Dijet 2012 на русском
Quick&Mini
MAX
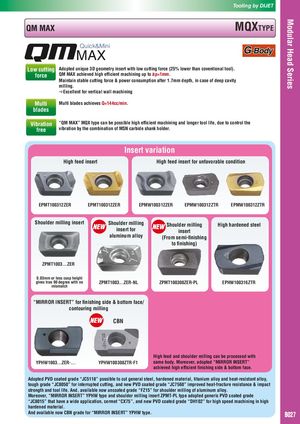
| Low cutting | Adopted unique 3D geometry insert with low cutting force (25% lower than coventional tool). |
| force | QM MAX achieved high efficient machining up to ap=1mm. |
| Maintain stable cutting force & power consumption after 1.7mm depth, in case of deep cavity | |
| milling. | |
| ÌExcellent for vertical wall machining | |
| Multi | Multi blades achieves Q=144cc/min. |
| blades | |
| Vibration | “QM MAX” MQX type can be possible high efficient machining and longer tool life, due to control the |
| free | vibration by the combination of MSN carbide shank holder. |
Insert variation
High feed insert High feed insert for unfavorable condition
EPMT100312ZER EPMT100312ZER EPMW100312ZER EPMW100312ZTR EPMW100312ZTR
Shoulder milling insert Shoulder milling
Shoulder milling High hardened steel
insert for insert
aluminum alloy (From semi-finishing
to finishing)
ZPMT1003...ZER
0.03mm or less cusp height
gives true 90 degree with no ZPMT1003...ZER-NL ZPMT100308ZER-PL EPHW100316ZTR
mismatch
“MIRROR INSERT” for finishing side & bottom face/
contouring milling
CBN
High feed and shoulder milling can be processed with
YPHW1003...ZER-... YPHW100308ZTR-F1 same body. Moreover, adopted “MIRROR INSERT”
achieved high efficient finishing side & bottom face. Adopted PVD coated grade “JC5118” possible to cut general steel, hardened material, titanium alloy and heat-resistant alloy, tough grade “JC8050” for interrupted cutting, and new PVD coated grade “JC7560” improved heat-fracture resistance & impact strength and tool life. And, available now uncoated grade “FZ15” for shoulder milling of aluminum alloy.
Moreover, “MIRROR INSERT” YPHW type and shoulder milling insert ZPMT-PL type adopted generic PVD coated grade “JC8015” that have a wide application, cermet “CX75”, and new PVD coated grade “DH102” for high speed machining in high hardened material. And available now CBN grade for “MIRROR INSERT” YPHW type. B027