Общий каталог Dijet 2018 - страница 32
Навигация
 Общий каталог Dijet 2012 на русском
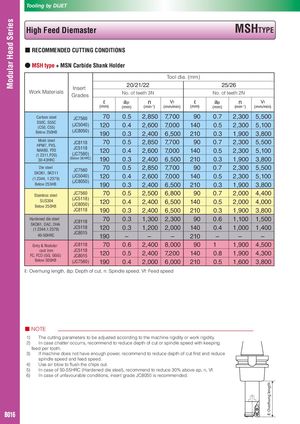
■ RECOMMENDED CUTTING CONDITIONS
- MSH type + MSN Carbide Shank Holder
Tooling by DIJET
| Tool dia | . (mm) | ||||||||
| Insert | 20/2 | 1/22 | 25 | /26 | |||||
| Work Materials | Grades | No. of | teeth 3N | No. of | teeth 2N | ||||
| ℓ (mm) | ap (mm) | n (min-1) | Vf (mm/min) | ℓ (mm) | ap (mm) | n (min-1) | Vf (mm/min) | ||
| Carbon steel | JC7560 | 70 | 0.5 | 2,850 | 7,700 | 90 | 0.7 | 2,300 | 5,500 |
| S50C, S55C (C50, C55) | (JC5040) | 120 | 0.4 | 2,600 | 7,000 | 140 | 0.5 | 2,300 | 5,100 |
| Below 250HB | (JC8050) | 190 | 0.3 | 2,400 | 6,500 | 210 | 0.3 | 1,900 | 3,800 |
| Mold steel HPM7 PX5 | JC8118 | 70 | 0.5 | 2,850 | 7,700 | 90 | 0.7 | 2,300 | 5,500 |
| , , NAK80, P20 (12311P20) | JC5118 (JC7560) | 120 | 0.4 | 2,600 | 7,000 | 140 | 0.5 | 2,300 | 5,100 |
| ., 30-43HRC | (Below 36HRC) | 190 | 0.3 | 2,400 | 6,500 | 210 | 0.3 | 1,900 | 3,800 |
| Die steel | JC7560 | 70 | 0.5 | 2,850 | 7,700 | 90 | 0.7 | 2,300 | 5,500 |
| SKD61, SKD11 (1.2344, 1.2379) | (JC5040) | 120 | 0.4 | 2,600 | 7,000 | 140 | 0.5 | 2,300 | 5,100 |
| Below 255HB | (JC8050) | 190 | 0.3 | 2,400 | 6,500 | 210 | 0.3 | 1,900 | 3,800 |
| Stainless steel | JC7560 | 70 | 0.5 | 2,500 | 6,800 | 90 | 0.7 | 2,000 | 4,400 |
| SUS304 Bl 250HB | (JC5118) (JC8050) | 120 | 0.4 | 2,400 | 6,500 | 140 | 0.5 | 2,000 | 4,000 |
| eow | JC8118 | 190 | 0.3 | 2,400 | 6,500 | 210 | 0.3 | 1,900 | 3,800 |
| Hardened die steel | JC8118 | 70 | 0.3 | 1,300 | 2,300 | 90 | 0.6 | 1,100 | 1,500 |
| SKD61, DAC, DHA (1.2344,1.2379) | JC5118 | 120 | 0.3 | 1,200 | 2,000 | 140 | 0.4 | 1,000 | 1,400 |
| 40-50HRC | JC8015 | 190 | – | – | – | 210 | – | – | – |
| Grey & Nodular | JC8118 | 70 | 0.6 | 2,400 | 8,000 | 90 | 1 | 1,900 | 4,500 |
| cast iron FC, FCD (GG, GGG) | JC5118 JC8015 | 120 | 0.5 | 2,400 | 7,200 | 140 | 0.8 | 1,900 | 4,300 |
| Below 300HB | (JC7560) | 190 | 0.4 | 2,000 | 6,000 | 210 | 0.5 | 1,600 | 3,800 |
| Hardened die steel | 70 | 0.2 | 2,380 | 2,610 | 70 | 0.4 | 1,300 | 1,600 | ||
| SKD61, DAC, DHA | a JC5118 | |||||||||
| ℓ: Overhung length, | p: Depth of cut, n: Spindle speed, Vf: Feed speed 1200.22,3802,380 | 120 | 0.3 | 1,200 | 1,400 | |||||
| (1.2344,1.2379) | JC8015 | |||||||||
| 40-50HRC | 160 | – | – | – 190 | – | – – | ||||
| Grey & Nodular | 70 | 0.5 | 2,980 | 6,550 | 70 | 0.6 | 2,400 | 5,800 | ||
| JC5118 | ||||||||||
| cast iron | JC8015 | 120 | 0.4 | 2,980 | 5,960 | 120 | 0.5 | 2,400 | 5,300 | |
| FC, FCD (GG, GGG) | (JC7560) | |||||||||
| Below 300HB | 160 | 0.3 | 2,500 | 5,000 | 190 | 0.4 | 2,000 | 4,800 |
ℓ : Overhung length, ap : Depth of cut, n : Spindle speed, Vf : Feed speed ■■ NOTE NOTE 1) ) The cutting parameters to be adjusted according to the machine rigidity or work rigidity.
1 The cutting parameters to be adjusted according to the machine rigidity or work rigidity. 2) In case chatter occurrs, recommend to reduce depth of cut or spindle speed with keeping 2)In case chatter occurrs, recommend to reduce depth of cut or spindle speed with keeping feed per tooth. 3) feed per tooth. If machine does not have enough power, recommend to reduce depth of cut first and reduce 3)If machine does not have enough power, recommend to reduce depth of cut first and reducespindle speed and feed speed. 4) spindle speed and feed speed.Use air blow to flush the chips out. 45) )Use air blow to flush the chips out.In case of 50-55HRC (Hardened die steel), recommend to reduce 30% above ap, n, Vf. 56) )In case of 50-55HRC (Hardened die steel), recommend to reduce 30% aboveIn case of unfavourable conditions, insert grade JC8050 is recommended. a , n, Vf. p 6)In case of unfavourable conditions, insert grade JC8050 is recommended.