Общий каталог Dijet 2018 - страница 27
Навигация
 Общий каталог Dijet 2012 на русском
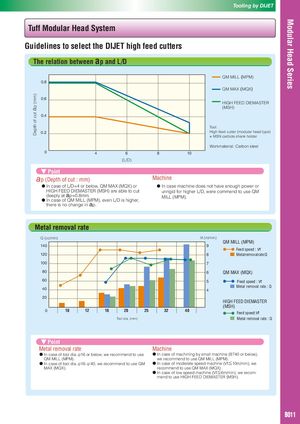
Guidelines to select the DIJET high feed cutters
The relation between ap and L/D
QM MILL (MPM) 0.8 QM MAX (MQX) 0.6 HIGH FEED DIEMASTER (MSH) 0.4
Tool: 0.2 High feed cutter (modular head type) + MSN carbide shank holder Workmaterial: Carbon steel 0 4 6 8 10 (L/D)
- Point
ap (Depth of cut : mm) Machine
- In case of L/D=4 or below, QM MAX (MQX) or
- In case machine does not have enough power or
HIGH FEED DIEMASTER (MSH) are able to cut unrigid for higher L/D, were commend to use QM deeply at ap=0.8mm. MILL (MPM).
- In case of QM MILL (MPM), even L/D is higher, there is no change in ap.
Metal removal rate
Q (cc/min) Vf (m/min) QM MILL (MPM) 140 9 Feed speed : Vf
| 120 | 8 | Metalremovalrate:Q | |
| 100 | 7 | ||
| 80 | 6 | QM MAX (MQX) | |
| 60 | 5 | Feed speed : Vf |
Metal removal rate : Q 40 4 20 HIGH FEED DIEMASTER
(MSH)
0 10 12 16 20 25 32 40
Feed speed:Vf Tool dia. (mm) Metal removal rate : Q
- Point
Metal removal rate Machine
- In case of tool dia.φ16 or below, we recommend to use
- In case of machining by small machine (BT40 or below),
QM MILL (MPM). we recommend to use QM MILL (MPM).
- In case of tool dia.φ16-φ40, we recommend to use QM
- In case of moderate speed machine (Vf≦10m/min), we
MAX (MQX). recommend to use QM MAX (MQX).
- In case of low speed machine (Vf≦6m/min), we recommend to use HIGH FEED DIEMASTER (MSH).