Общий каталог Dijet 2018 - страница 24
Навигация
 Общий каталог Dijet 2012 на русском
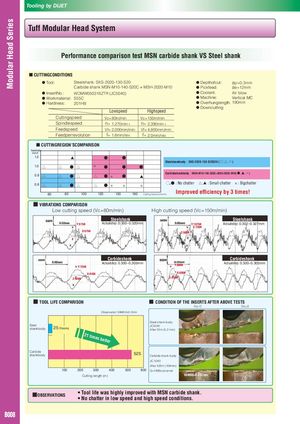
Performance comparison test MSN carbide shank VS Steel shank
- CUTTINGCONDITIONS
- Tool: Steelshank: SKS-2020-130-S20
- Depthofcut: ap=0.3mm
Carbide shank MSN-M10-140-S20C + MSH-2020-M10 Pickfeed: ae=12mm
- InsertNo.: WDMW050316ZTR (JC5040)
- Coolant: Air blow
- Workmaterial: S55C
- Machine: Vertical MC
- Hardness: 201HB
- Overhunglength: 190mm
- Downcutting
Lowspeed Highspeed
| Cuttingspeed | Vc= 80m/min | Vc= 150m/min | ||
| Spindlespeed | n= 1,270min | n= 2,390min | ||
| -1 | -1 | |||
| Feedspeed | Vf= 2,000mm/min | Vf= 4,800mm/min | ||
| Feedperrevolution | f= 1.6mm/rev | f= 2.0mm/rev |
- CUTTINGREGION’SCOMPARISON
feedrate mm/t
| 1.2 | ▲ | ● | ● | |||||
| Steelshankbody : SKS-2020-130-S20S20 (○ ,△,×) | ||||||||
| 1.0 | △ △ | ● △ | × | ● | ● | ● | ||
| Carbideshankbody : MSN-M10-140-S20C+MSH-2020-M10(●,▲,×) | ||||||||
| 0.8 △ | △ | ● △ | △ | ● | × | ● | ▲ | |
| ○,● : No chatter △,▲ : Small chatter × : Bigchatter | ||||||||
| 0.6 △ | △ | ● △ | △ | ● | × | × | × | |
| Improved efficiency by 3 times! |
60 80 100 120 150 180 Cutting Speed (m/min)
- VIBRATIONS COMPARISON Low cutting speed (Vc=80m/min) High cutting speed (Vc=150m/min)
Steelshank Steelshank
Y:975N Actualstep: 0.300–0.320mm Y:1075N Actualstep: 0.302–0.327mm
X:720N X:575N Z:500N
Carbideshank Carbideshank Actualstep: 0.300–0.305mm Actualstep: 0.300–0.305mm Y:800N Y:725N X:410N X:430N Z:420N Z:470N
- TOOL LIFE COMPARISON
- CONDITION OF THE INSERTS AFTER ABOVE TESTS
〈No.1〉 〈 No.2〉 Observation:V BMAX >0.2mm
Steel shank body Steel JC5040 25 Chipping shankbody After 25m (5.2 min) 21 times better
Carbide 525 shankbody Carbide shank body JC 5040 After 525m (109min) 100 200 300 400 500 600 Q=1890cc/corner Cutting length (m) VBMAX=0.202mm
- Tool life was highly improved with MSN carbide shank.
■OBSERVATIONS
- No chatter in low speed and high speed conditions.