Каталог Tungaloy глубокое сверление 2 - страница 20
Навигация
 Каталог Tungaloy инструмент для автоматов швейцарского типа
 Общий каталог Tungaloy 2020 - 2021
 Каталог Tungaloy зубофрезерование
 Брошюра Tungaloy новая продукция
 Каталог Tungaloy глубокое сверление 1
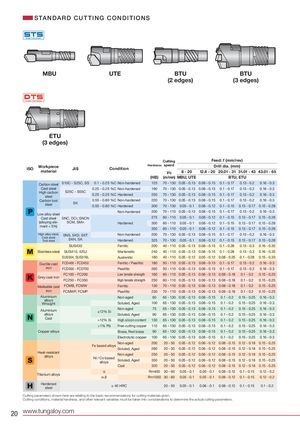
STANDARD CUTTING CONDITIONS
MBU UTE BTU BTU
(2 edges) (3 edges)
ETU
(3 edges)
| Cutting | Fe | ed:f (mm/r | ev) | ||||||||
| ISO | Workpiece | JIS | Co | ndition | Hardnes | s speed | D | rill dia.(m | m) | ||
| material | (HB) | Vc (m/min) | 8 - 20 MBU, UTE | 12.6 - 20 | 20.01 - 31 BTU | 31.01 - 43 , ETU | 43.01 - 65 | ||||
| Carbon steel | S10C - S25C, SS | 0.1 - 0.25 % | C Non-hardened | 125 | 70 - 130 | 0.05 - 0.13 | 0.08 - 0.15 | 0.1 - 0.17 | 0.13 - 0.2 | 0.16 - 0.3 | |
| Cast steel | S25C - S55C | 0.25 - 0.25 % | C Non-hardened | 190 | 70 - 130 | 0.05 - 0.13 | 0.08 - 0.15 | 0.1 - 0.17 | 0.13 - 0.2 | 0.16 - 0.3 | |
| High carbon steel | 0.25 - 0.25 % | C Hardened | 250 | 70 - 130 | 0.05 - 0.13 | 0.08 - 0.15 | 0.1 - 0.17 | 0.13 - 0.2 | 0.16 - 0.3 | ||
| Carbon tool | SK | 0.55 - 0.80 % | C Non-hardened | 220 | 70 - 130 | 0.05 - 0.13 | 0.08 - 0.15 | 0.1 - 0.17 | 0.13 - 0.2 | 0.16 - 0.3 | |
| steel | 0.55 - 0.80 % | C Hardened | 300 | 70 - 130 | 0.05 - 0.1 | 0.08 - 0.12 | 0.1 - 0.15 | 0.13 - 0.17 | 0.15 - 0.28 | ||
| Low allo steel | Non-hardened | 200 | 70 - 110 | 0.05 - 0.13 | 0.08 - 0.15 | 0.1 - 0.17 | 0.13 - 0.2 | 0.16 - 0.3 | |||
| y Cast steel | SNC, DCr, SNCN | 275 | 60 - 110 | 0.05 - 0.1 | 0.08 - 0.12 | 0.1 - 0.15 | 0.13 - 0.17 | 0.15 - 0.28 | |||
| (alloying ele- | SCM, SMn | Hardened | 300 | 60 - 110 | 0.05 - 0.1 | 0.08 - 0.12 | 0.1 - 0.15 | 0.13 - 0.17 | 0.15 - 0.28 | ||
| ment < 5%) | 350 | 60 - 110 | 0.05 - 0.1 | 0.08 - 0.12 | 0.1 - 0.15 | 0.13 - 0.17 | 0.15 - 0.28 | ||||
| High alloy steel, | SNS, SKD, SKT | Non-hardened | 200 | 70 - 130 | 0.05 - 0.13 | 0.08 - 0.15 | 0.1 - 0.17 | 0.13 - 0.2 | 0.16 - 0.3 | ||
| Cast steel Tool steel | SKH, SK | Hardened | 325 | 70 - 130 | 0.05 - 0.1 | 0.08 - 0.12 | 0.1 - 0.15 | 0.13 - 0.17 | 0.15 - 0.28 | ||
| SUS430 | Ferritic | 200 | 40 - 110 | 0.05 - 0.13 | 0.08 - 0.15 | 0.1 - 0.28 | 0.13 - 0.3 | 0.16 - 0.35 | |||
| Stainless steel | SUS410, 420J | Martensitic | 240 | 40 - 110 | 0.05 - 0.13 | 0.08 - 0.15 | 0.1 - 0.28 | 0.13 - 0.3 | 0.16 - 0.35 | ||
| SUS304, SUS316L | Austenitic | 180 | 40 - 110 | 0.05 - 0.12 | 0.05 - 0.12 | 0.08 - 0.25 | 0.1 - 0.28 | 0.15 - 0.33 | |||
| Ductile cast | FCD400 - FCD450 | Ferritic / Pearlitic | 180 | 50 - 110 | 0.05 - 0.13 | 0.08 - 0.15 | 0.1 - 0.17 | 0.13 - 0.2 | 0.16 - 0.3 | ||
| iron | FCD500 - FCD700 | Pearlitic | 260 | 50 - 110 | 0.05 - 0.13 | 0.08 - 0.15 | 0.1 - 0.17 | 0.13 - 0.2 | 0.16 - 0.3 | ||
| FC100 - FC200 | Low tensile strength | 160 | 60 - 110 | 0.05 - 0.13 | 0.06 - 0.13 | 0.08 - 0.18 | 0.1 - 0.2 | 0.15 - 0.25 | |||
| Grey cast iron | FC250 - FC350 | High tensile strength | 250 | 60 - 110 | 0.05 - 0.13 | 0.06 - 0.13 | 0.08 - 0.18 | 0.1 - 0.2 | 0.15 - 0.25 | ||
| Malleable cast | FCMB, FCMW | Ferritic | 130 | 70 - 110 | 0.05 - 0.13 | 0.06 - 0.13 | 0.08 - 0.18 | 0.1 - 0.2 | 0.15 - 0.25 | ||
| iron | FCMWP, FCMP | Pearlitic | 230 | 70 - 110 | 0.05 - 0.13 | 0.06 - 0.13 | 0.08 - 0.18 | 0.1 - 0.2 | 0.15 - 0.25 | ||
| Aluminium | Non-aged | 60 | 65 - 130 | 0.05 - 0.13 | 0.08 - 0.15 | 0.1 - 0.2 | 0.15 - 0.25 | 0.16 - 0.3 | |||
| alloys Wrought | Soluted, Aged | 100 | 65 - 130 | 0.05 - 0.13 | 0.08 - 0.15 | 0.1 - 0.2 | 0.15 - 0.25 | 0.16 - 0.3 | |||
| Aluminium | 12% Si | Non-aged | 75 | 65 - 130 | 0.05 - 0.13 | 0.08 - 0.15 | 0.1 - 0.2 | 0.15 - 0.25 | 0.16 - 0.3 | ||
| alloys | ≤ | Soluted, Aged | 90 | 65 - 130 | 0.05 - 0.13 | 0.08 - 0.15 | 0.1 - 0.2 | 0.15 - 0.25 | 0.16 - 0.3 | ||
| Cast | >12% Si | High silicon content | 130 | 65 - 130 | 0.05 - 0.13 | 0.08 - 0.15 | 0.1 - 0.2 | 0.15 - 0.25 | 0.16 - 0.3 | ||
| >1% Pb | Free-cutting copper | 110 | 65 - 130 | 0.05 - 0.13 | 0.08 - 0.15 | 0.1 - 0.2 | 0.15 - 0.25 | 0.16 - 0.3 | |||
| Copper alloys | Brass, Red brass | 90 | 65 - 130 | 0.05 - 0.13 | 0.08 - 0.15 | 0.1 - 0.2 | 0.15 - 0.25 | 0.16 - 0.3 | |||
| Electrolytic copper | 100 | 65 - 130 | 0.05 - 0.13 | 0.08 - 0.15 | 0.1 - 0.2 | 0.15 - 0.25 | 0.16 - 0.3 | ||||
| F bd ll | Non-aged | 200 | 20 - 50 | 0.05 - 0.12 | 0.06 - 0.12 | 0.08 - 0.15 | 0.12 - 0.18 | 0.15 - 0.25 | |||
| e ase aoy | Soluted, Aged | 280 | 20 - 50 | 0.05 - 0.12 | 0.06 - 0.12 | 0.08 - 0.15 | 0.12 - 0.18 | 0.15 - 0.25 | |||
| Heat-resistant ll | Non-aged | 250 | 20 - 50 | 0.05 - 0.12 | 0.06 - 0.12 | 0.08 - 0.15 | 0.12 - 0.18 | 0.15 - 0.25 | |||
| aoys | Ni / Co based allos | Soluted, Aged | 350 | 20 - 50 | 0.05 - 0.12 | 0.06 - 0.12 | 0.08 - 0.15 | 0.12 - 0.18 | 0.15 - 0.25 | ||
| y | Cast | 320 | 20 - 50 | 0.05 - 0.12 | 0.06 - 0.12 | 0.08 - 0.15 | 0.12 - 0.18 | 0.15 - 0.25 | |||
| α | Rm400 | 30 - 60 | 0.05 - 0.1 | 0.05 - 0.1 | 0.08 - 0.12 | 0.1 - 0.15 | 0.12 - 0.2 | ||||
| Titanium alloys | α-β | Rm1050 | 30 - 60 | 0.05 - 0.1 | 0.05 - 0.1 | 0.08 - 0.12 | 0.1 - 0.15 | 0.12 - 0.2 | |||
| Hardened steel | ≥ | 40 HRC | 20 - 50 | 0.05 - 0.1 | 0.06 - 0.1 | 0.08 - 0.12 | 0.1 - 0.15 | 0.1 - 0.2 |
Cutting parameters shown here are relating to the basic recommendations for cutting materials given. Cutting conditions, material hardness, and other relevant variables must be taken into considerations to determine the actual cutting parameters.