Общий каталог Sumitomo 2018 - 2019 - страница 70
Навигация
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части
- Pages 3-6_CS6_EN_web
- A 1-20 insert selection EN_web
- B 1-14 grades_EN_web
- C01-17 inserts intro pages_EN_web
- C18-56 negative inserts_EN_web
- C57-86 positive inserts_EN_web
- D 1-46 tool holders_EN_web
- E 1-24 boring bars_EN_web
- F 1-48 grooving_thread tools_EN_web
- G 1-54 milling cutters_EN_web
- H 1-48 insert type endmills_EN_web
- J 1-24 new endmills_EN_web
- J 25-50 endmills_EN_web
- K 1-46 Multi-Drills_EN_web
- K 47-76 Multi-Drills_EN_web
- L 1-28 cbn_pcd grades_EN_web
- M 1-34 cbn_pcd inserts_EN_web
- M 35-56 SHM tools_EN_web
- N1-24 technical guidance_EN_web
- P 1-8 spare parts_neu_EN_web
- P 9-22 index_notes_EN_web
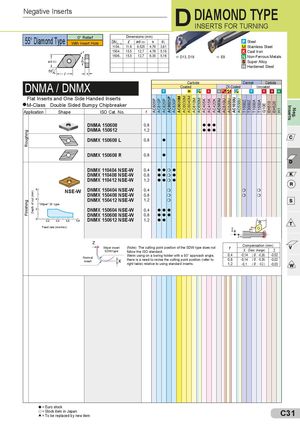
55° Diamond Type 0° Relief Dimensions (mm)
| With Insert Hole DN_ _ | l | ød | s d | PP Steel |
| (IC) | 1 | |||
| 1104.. | 11,6 | 9,525 | 4,76 3,81 | MM Stainless Steel |
| 1504.. 15,5 | 12,7 | 4,76 5,16 | KK Cast Iron | |
| 1506.. 15,5 | 12,7 | 6,35 5,16 | a E9 a D13, D19 NN Non-Ferrous Metals | |
| SS Super Alloy | ||||
| HH Hardened Steel |
DNMA / DNMX Carbide Cermet Carbide
Coated ZX-Coated Uncoated
| P | M | P | K | H | K | M | P | P | K | S | N | |
| M | S | S | M | |||||||||
| Flat Inserts and One Side Handed Inserts | ||||||||||||
| M-Class Double Sided Bumpy Chipbreaker |
| Shape Application | ISO Cat. No. r | AC530U T1500Z T3000Z T1000A T1500A G10E EH510 EH520 H1 AC510U AC520U AC6030M AC6040M AC610M AC630M AC405K AC415K AC420K AC805P AC810P AC820P | |
| DNMA 150608 | 0,8 | l l l | |
| DNMA 150612 | 1,2 | l l l | |
| DNMX 150608 L | 0,8 | l | |
| DNMX 150608 R | 0,8 | l | |
| DNMX 110404 NSE-W | 0,4 | l l m l | |
| DNMX 110408 NSE-W | 0,8 | l l m l | |
| DNMX 110412 NSE-W | 1,2 | l l m l | |
| NSE-W DNMX 150404 NSE-W | 0,4 | m m m | |
| DNMX 150408 NSE-W | 0,8 | m m m | |
| DNMX 150412 NSE-W | 1,2 | m | |
| ”Wiper” W type | |||
| DNMX 150604 NSE-W | 0,4 | l l l | |
| DNMX 150608 NSE-W | 0,8 | l l l | |
| DNMX 150612 NSE-W | 1,2 | l l | |
| Feed rate (mm/rev) | |||
| (Note) The cutting point position of the SDW type does not | Compensation (mm) r | ||
| Wiper insert | (Diam. change) Z X | ||
| follow the ISO standard. SDW type | |||
| Wenn using on a boring holder with a 93° approach angle, | -0,14 ( Ø : -0,28) -0,02 0,4 | ||
| Normal | there is a need to revise the cutting point position (refer to | -0,14 ( Ø : -0,28) -0,02 0,8 |
insert right table) relative to using standard inserts. 1,2 -0,1 ( Ø : -0,2 ) -0,03