Общий каталог Sumitomo 2018 - 2019 - страница 377
Навигация
 Общий каталог Sumitomo 2012
 Каталог Sumitomo резьбонарезной инструмент
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo запасные части
- Pages 3-6_CS6_EN_web
- A 1-20 insert selection EN_web
- B 1-14 grades_EN_web
- C01-17 inserts intro pages_EN_web
- C18-56 negative inserts_EN_web
- C57-86 positive inserts_EN_web
- D 1-46 tool holders_EN_web
- E 1-24 boring bars_EN_web
- F 1-48 grooving_thread tools_EN_web
- G 1-54 milling cutters_EN_web
- H 1-48 insert type endmills_EN_web
- J 1-24 new endmills_EN_web
- J 25-50 endmills_EN_web
- K 1-46 Multi-Drills_EN_web
- K 47-76 Multi-Drills_EN_web
- L 1-28 cbn_pcd grades_EN_web
- M 1-34 cbn_pcd inserts_EN_web
- M 35-56 SHM tools_EN_web
- N1-24 technical guidance_EN_web
- P 1-8 spare parts_neu_EN_web
- P 9-22 index_notes_EN_web
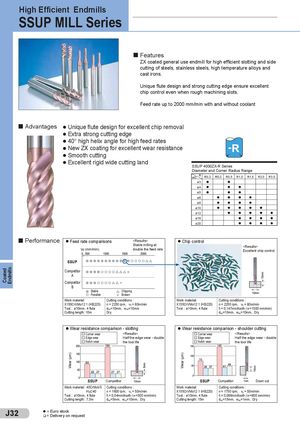
High Efficient Endmills
SSUP MILL Series
Features
ZX coated general use endmill for high efficient slotting and side
cutting of steels, stainless steels, high temperature alloys and
cast irons.
Unique flute design and strong cutting edge ensure excellent
chip control even when rough machining slots.
Feed rate up to 2000 mm/min with and without coolant
Advantages Unique flute design for excellent chip removal
l
Extra strong cutting edge
l
40° high helix angle for high feed rates
l
New ZX coating for excellent wear resistance
l
Smooth cutting
l
Excellent rigid wide cutting land
l
SSUP 4000ZX-R Series Diameter and Corner Radius Range
| R | R0,2 | R0,3 | R0,5 | R1,0 | R1,5 | R2.0 | R3.0 |
| øD | |||||||
| ø3 | l | l | |||||
| ø4 | l | l | l | ||||
| ø5 | l | l | l | ||||
| ø6 | l | l | l | l | |||
| ø8 | l | l | l | l | |||
| ø10 | l | l | l | l | l | ||
| ø12 | l | l | l | l | l | ||
| ø16 | l | l | l | l | |||
| ø20 | l | l | l | l |
Performance Feed rate comparisons <Results> Chip control
l l Stable milling at <Results> vf (mm/min) double the feed rate Excellent chip control
SSUP
Competitor
A
Competitor
B
Stable Chipping Possible Broken
| Work material: | Cutting conditions : | Work material: | Cutting conditions : | ||
| X155CrVMo12 1 (HB220) | n = 2250 rpm, v = 80m/min | X155CrVMo12 1 (HB220) | n = 2250 rpm, v = 80m/min | ||
| c | c | ||||
| Tool : ø10mm, 4 flute | d =10mm, w | =10mm | Tool : ø10mm, 4 flute | f = 0,147mm/tooth (v =1500 mm/min) | |
| oc | oc | t | f | ||
| Cutting length: 10m | Dry | d =10mm, w | =10mm, Dry | ||
| oc | oc | ||||
| l Wear resistance comparison - slotting | l Wear resistance comparison - shoulder cutting |
| Corner wear | <Results> | Corner wear | <Results> |
| Edge wear | Half the edge wear - double | Edge wear | Half the edge wear - double |
| Notch wear | the tool life | Notch wear | the tool life |
| SSUP | Competitor | SSUP | Competitor | Down cut | ||
| Work material: 40CrMoV5 | Cutting conditions : | Work material: | Cutting conditions : | |||
| HRC40 | n = 1600 rpm, vc = 50m/min | X155CrVMo12 1 (HB220) | n = 1750 rpm, vc = 55m/min | |||
| Tool : ø10mm, 4 flute | ft = 0,04mm/tooth (vf =500 mm/min) | Tool : ø10mm, 4 flute | ft = 0,086mm/tooth (vf =600 mm/min) | |||
| Cutting length: 7,5m | doc=5mm, woc=10mm, Dry | Cutting length: 15m | doc=15mm, woc=1mm, Dry |