Общий каталог Mitsubishi 2020 - 2021 - страница 1111
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
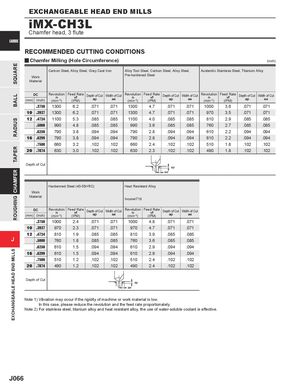
iMX-CH3L
Chamfer head, 3 flute
CARBIDE
RECOMMENDED CUTTING CONDITIONS
| y C | amfe | r Milling | (Hole C | ircumfe | rence) | (inch) | |||||||
| W Mat | ork erial | Carbon Ste | el, Alloy Stee | l, Gray Cast | Iron | Alloy Tool St Pre-hardene | eel, Carbon d Steel | Steel, Alloy | Steel, | Austenitic S | tainless Ste | el, Titanium | Alloy |
| D (mm) | C (inch) | Revolution n (min-1) | Feed Rate vf (IPM) | Depth of Cut ap | Width of Cut ae | Revolution n (min-1) | Feed Rate vf (IPM) | Depth of Cut ap | Width of Cut ae | Revolution n (min-1) | Feed Rate vf (IPM) | Depth of Cut ap | Width of Cut ae |
| .3750 | 1300 | 6.2 | .071 | .071 | 1300 | 4.7 | .071 | .071 | 1000 | 3.6 | .071 | .071 | |
| 10 | .3937 | 1300 | 6.2 | .071 | .071 | 1300 | 4.7 | .071 | .071 | 970 | 3.5 | .071 | .071 |
| 12 | .4724 | 1100 | 5.3 | .085 | .085 | 1100 | 4.0 | .085 | .085 | 810 | 2.9 | .085 | .085 |
| .5000 | 990 | 4.8 | .085 | .085 | 990 | 3.6 | .085 | .085 | 760 | 2.7 | .085 | .085 | |
| .6250 | 790 | 3.8 | .094 | .094 | 790 | 2.8 | .094 | .094 | 610 | 2.2 | .094 | .094 | |
| 16 | .6299 | 790 | 3.8 | .094 | .094 | 790 | 2.8 | .094 | .094 | 610 | 2.2 | .094 | .094 |
| .7500 | 660 | 3.2 | .102 | .102 | 660 | 2.4 | .102 | .102 | 510 | 1.8 | .102 | .102 | |
| 20 | .7874 | 630 | 3.0 | .102 | .102 | 630 | 2.3 | .102 | .102 | 490 | 1.8 | .102 | .102 |
| W Mat Depth | ork erial of Cut | Hardenned | Steel (40-55 | HRC) | Heat Resist Inconel718 | ant Alloy | ap ae | ||||||
| D | C | Revolution | Feed Rate f | Depth of Cut | Width of Cut | Revolution | Feed Rate f | Depth of Cut | Width of Cut | ||||
| (mm) | (inch) | n (min-1) | v (IPM) | ap | ae | n (min-1) | v (IPM) | ap | ae | ||||
| .3750 | 1000 | 2.4 | .071 | .071 | 1000 | 4.8 | .071 | .071 | |||||
| 10 | .3937 | 970 | 2.3 | .071 | .071 | 970 | 4.7 | .071 | .071 | ||||
| 12 | .4724 | 810 | 1.9 | .085 | .085 | 810 | 3.9 | .085 | .085 | ||||
| .5000 | 760 | 1.8 | .085 | .085 | 760 | 3.6 | .085 | .085 | |||||
| .6250 | 610 | 1.5 | .094 | .094 | 610 | 2.9 | .094 | .094 | |||||
| 16 | .6299 | 610 | 1.5 | .094 | .094 | 610 | 2.9 | .094 | .094 | ||||
| .7500 | 510 | 1.2 | .102 | .102 | 510 | 2.4 | .102 | .102 | |||||
| 20 | .7874 | 490 | 1.2 | .102 | .102 | 490 | 2.4 | .102 | .102 | ||||
| Depth | of Cut | ap ae |
Note 1) Vibration may occur if the rigidity of machine or work material is low. In this case, please reduce the revolution and the feed rate proportionately. Note 2) For stainless steel, titanium alloy and heat resistant alloy, the use of water-soluble coolant is effective.