Общий каталог Dijet 2018 - страница 66
Навигация
 Общий каталог Dijet 2012 на русском
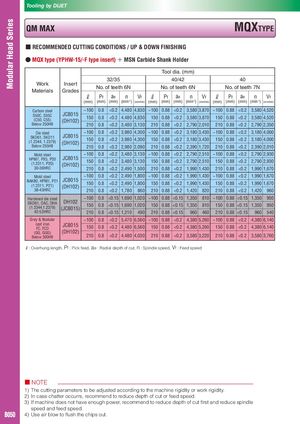
■ RECOMMENDED CUTTING CONDITIONS / UP & DOWN FINISHING
- MQX type (YPHW-15/-F type insert) + MSN Carbide Shank Holder
| Tool | dia.( | mm) | ||||||||||||||
| 32/35 | 40/42 | 40 | ||||||||||||||
| Work Materials | Insert Grades | No. | of teet | h6N | No. | of teet | h6N | No. o | f teet | h7N | ||||||
| ℓ (mm) | Pf (mm) | ae (mm) | n (min-1) | Vf (mm/min) | ℓ (mm) | Pf (mm) | ae (mm) | n (min-1) | Vf (mm/min) | ℓ (mm) | Pf (mm) | ae (mm) | n (min-1) | Vf (mm/min) | ||
| Carbon steel | JC801 | ~100 | 0.8 | 4,480 | 4,830 | ~100 | 0.88 | 3,580 | 3,870 | ~100 | 0.88 | 3,580 | 4,520 | |||
| S50C, S55C (C50, C55) | 5 (DH102) | 150 | 0.8 | 4,480 | 4,830 | 150 | 0.88 | 3,580 | 3,870 | 150 | 0.88 | 3,580 | 4,520 | |||
| Below 250HB | 210 | 0.8 | 3,480 | 3,130 | 210 | 0.88 | 2,790 | 2,010 | 210 | 0.88 | 2,790 | 2,350 | ||||
| Die steel | ~100 | 0.8 | 3,980 | 4,300 | ~100 | 0.88 | 3,180 | 3,430 | ~100 | 0.88 | 3,180 | 4,000 | ||||
| SKD61, SKD11 (1.2344, 1.2379) | JC8015 (DH102) | 150 | 0.8 | 3,980 | 4,300 | 150 | 0.88 | 3,180 | 3,430 | 150 | 0.88 | 3,180 | 4,000 | |||
| Below 255HB | 210 | 0.8 | 2,980 | 2,090 | 210 | 0.88 | 2,390 | 1,720 | 210 | 0.88 | 2,390 | 2,010 | ||||
| Mold steel | 1 | ~100 | 0.8 | 3,480 | 3,130 | ~100 | 0.88 | 2,790 | 2,510 | ~100 | 0.88 | 2,790 | 2,930 | |||
| HPM7, PX5, P20 (1.2311, P20) | JC805 (DH102) | 150 | 0.8 | 3,480 | 3,130 | 150 | 0.88 | 2,790 | 2,510 | 150 | 0.88 | 2,790 | 2,930 | |||
| 30-36HRC | 210 | 0.8 | 2,490 | 1,500 | 210 | 0.88 | 1,990 | 1,430 | 210 | 0.88 | 1,990 | 1,670 | ||||
| Mold steel | ~100 | 0.8 | 2,490 | 1,800 | ~100 | 0.88 | 1,990 | 1,430 | ~100 | 0.88 | 1,990 | 1,670 | ||||
| NAK80, HPM1, P21 (1.2311, P21) | JC8015 (DH102) | 150 | 0.8 | 2,490 | 1,800 | 150 | 0.88 | 1,990 | 1,430 | 150 | 0.88 | 1,990 | 1,670 | |||
| 38-43HRC | 210 | 0.8 | 1,780 | 860 | 210 | 0.88 | 1,420 | 820 | 210 | 0.88 | 1,420 | 960 | ||||
| Hardened die steel | ~100 | 0.8 | 1,690 | 1,020 | ~100 | 0.88 | 1,350 | 810 | ~100 | 0.88 | 1,350 | 950 | ||||
| SKD61, DAC, DHA (1.2344,1.2379) | DH102 (JC8015) | 150 | 0.8 | 1,690 | 1,020 | 150 | 0.88 | 1,350 | 810 | 150 | 0.88 | 1,350 | 950 | |||
| 42-52HRC | 210 | 0.8 | 1,210 | 490 | 210 | 0.88 | 960 | 460 | 210 | 0.88 | 960 | 540 | ||||
| Grey & Nodular | ~100 | 0.8 | 5,470 | 6,560 | ~100 | 0.88 | 4,380 | 5,260 | ~100 | 0.88 | 4,380 | 6,140 | ||||
| cast iron FC, FCD | JC8015 | 150 | 0.8 | 4,480 | 6,560 | 150 | 0.88 | 4,380 | 5,260 | 150 | 0.88 | 4,380 | 6,140 | |||
| (GG, GGG) Below 300HB | (DH102) | 210 | 0.8 | 4,480 | 4,030 | 210 | 0.88 | 3,580 | 3,220 | 210 | 0.88 | 3,580 | 3,760 |