Общий каталог Dijet 2018 - страница 64
Навигация
 Общий каталог Dijet 2012 на русском
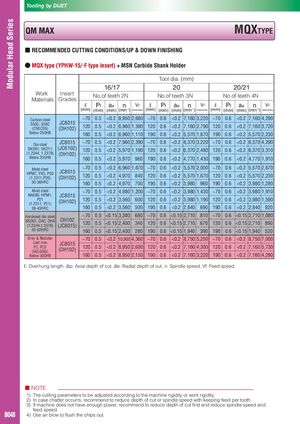
■ RECOMMENDED CUTTING CONDITIONS/UP & DOWN FINISHING
- MQX type (YPHW-15/-F type insert) + MSN Carbide Shank Holder
| Tool | dia. | (mm) | ||||||||||||||
| 16/1 | 7 | 20 | 20/2 | 1 | ||||||||||||
| Work Materials | Insert Grades | No.o | f teet | h2N | No.o | f teet | h3N | No.o | f tee | th4N | ||||||
| ℓ (mm) | Pf (mm) | ae (mm) | n (min-1) | Vf (mm/min) | ℓ (mm) | Pf (mm) | ae (mm) | n (min-1) | Vf (mm/min) | ℓ (mm) | Pf (mm) | ae (mm) | n (min-1) | Vf (mm/min) | ||
| Carbon steel | ~70 | 0.5 | 8,950 | 2,680 | ~70 | 0.6 | 7,160 | 3,220 | ~70 | 0.6 | 7,160 | 4,290 | ||||
| S50C, S55C (C50,C55) | JC8015 (DH102) | 120 | 0.5 | 6,960 | 1,390 | 120 | 0.6 | 7,160 | 2,790 | 120 | 0.6 | 7,160 | 3,720 | |||
| Below 250HB | 160 | 0.5 | 6,960 | 1,110 | 190 | 0.6 | 5,570 | 1,670 | 190 | 0.6 | 5,570 | 2,230 | ||||
| Die steel | JC8015 | ~70 | 0.5 | 7,960 | 2,390 | ~70 | 0.6 | 6,370 | 3,220 | ~70 | 0.6 | 6,370 | 4,290 | |||
| SKD61, SKD11 (1.2344, 1.2379) | (JC6102) (DH102) | 120 | 0.5 | 5,970 | 1,190 | 120 | 0.6 | 6,370 | 2,480 | 120 | 0.6 | 6,370 | 3,310 | |||
| Below 255HB | 160 | 0.5 | 5,970 | 960 | 190 | 0.6 | 4,770 | 1,430 | 190 | 0.6 | 4,770 | 1,910 | ||||
| Mold steel | ~70 | 0.5 | 6,960 | 1,670 | ~70 | 0.6 | 5,570 | 2,000 | ~70 | 0.6 | 5,570 | 2,670 | ||||
| HPM7, PX5, P20 (1.2311,P20) | JC8015 (DH102) | 120 | 0.5 | 4,970 | 840 | 120 | 0.6 | 5,570 | 1,670 | 120 | 0.6 | 5,570 | 2,230 | |||
| 30-36HRC | 160 | 0.5 | 4,970 | 700 | 190 | 0.6 | 3,980 | 960 | 190 | 0.6 | 3,980 | 1,280 | ||||
| Mold steel NAK80 HPM1 | ~70 | 0.5 | 4,980 | 1,200 | ~70 | 0.6 | 3,980 | 1,430 | ~70 | 0.6 | 3,980 | 1,910 | ||||
| , , P21 | JC8015 (DH102) | 120 | 0.5 | 3,560 | 600 | 120 | 0.6 | 3,980 | 1,190 | 120 | 0.6 | 3,980 | 1,590 | |||
| (1.2311, P21) 38-43HRC | 160 | 0.5 | 3,560 | 500 | 190 | 0.6 | 2,840 | 690 | 190 | 0.6 | 2,840 | 920 | ||||
| Hardened die steel | ~70 | 0.5 | 3,380 | 680 | ~70 | 0.6 | 2,710 | 810 | ~70 | 0.6 | 2,710 | 1,080 | ||||
| SKD61, DAC, DHA (1.2344,1.2379) | DH102 (JC8015) | 120 | 0.5 | 2,400 | 340 | 120 | 0.6 | 2,710 | 670 | 120 | 0.6 | 2,710 | 890 | |||
| 42-52HRC | 160 | 0.5 | 2,400 | 280 | 190 | 0.6 | 1,940 | 390 | 190 | 0.6 | 1,940 | 520 | ||||
| Grey & Nodular t i | ~70 | 0.5 | 10,900 | 4,360 | ~70 | 0.6 | 8,750 | 5,250 | ~70 | 0.6 | 8,750 | 7,000 | ||||
| cas ron FC, FCD | JC8015 (DH102) | 120 | 0.5 | 8,950 | 2,680 | 120 | 0.6 | 7,160 | 4,300 | 120 | 0.6 | 7,160 | 5,730 | |||
| (GG,GGG) Below 300HB | 160 | 0.5 | 8,950 | 2,150 | 190 | 0.6 | 7,160 | 3,220 | 190 | 0.6 | 7,160 | 4,290 |